OPEN FROM 9AM TO 5PM – CLOSED ON WEEKENDS

How to Choose a China Top OEM Optical Sight Factory?

Choosing a China Top Oem Optical Sight Factory requires more than comparing prices or viewing attractive product photos. It demands evidence of engineering discipline, production consistency, and responsible business practices. Grand View Research reports continued growth in the global optical instruments market, driven by precision manufacturing, outdoor recreation, and professional observation applications. This trend creates opportunity, but it also increases supplier risk. A polished catalog proves little.

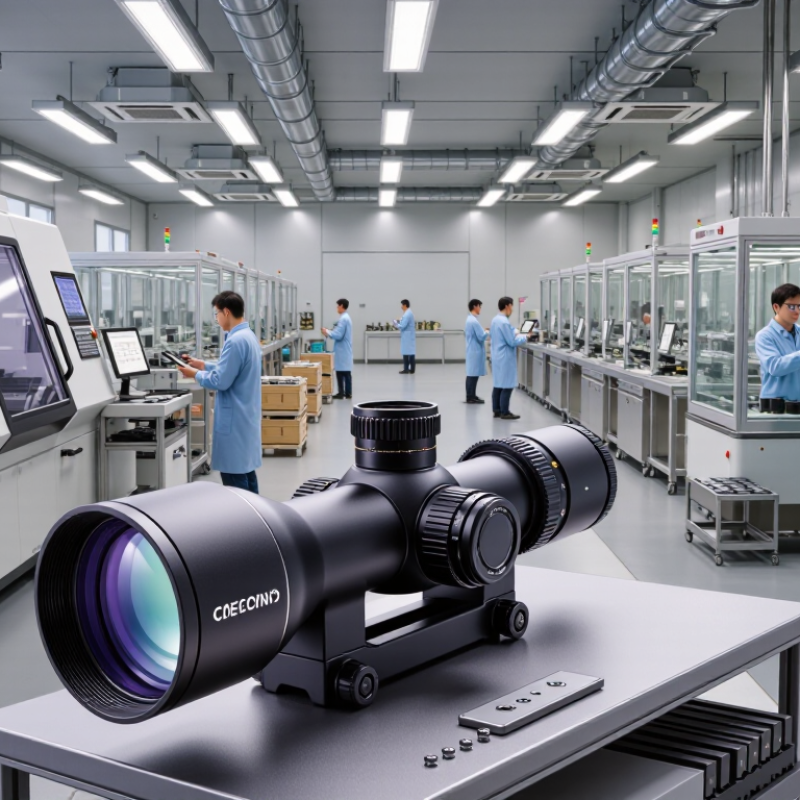
A qualified Oem Optical Sight Factory should demonstrate clear control over lens grinding, multilayer coating, sealing, alignment, and final inspection. Ask for measurable data, including optical clarity, light transmission, parallax performance, shock resistance, waterproof testing, and temperature-cycle results. Factory experience matters. A supplier should provide traceable samples, inspection records, calibration certificates, and documented corrective actions. ISO 9001 certification can support process reliability, although certification alone cannot replace an independent audit. Look closely at the workshop floor. Are lenses protected from dust? Are torque tools calibrated? Can operators explain their inspection standards?

Industry research from Mordor Intelligence and Fortune Business Insights also highlights rising demand for durable, compact, and digitally integrated optical products. Buyers should therefore assess both current capacity and future engineering support. Confirm prototype lead times, minimum order quantities, tooling ownership, packaging controls, and after-sales response. Do not ignore regulatory requirements. Product classification, export documentation, labeling, and destination-country laws must be reviewed before any shipment.

The decision is rarely perfect. Supplier scorecards can miss hidden weaknesses. An on-site audit may reveal more than months of emails. Choose evidence over promises, while leaving room for careful improvement.

How to Choose a China Top OEM Optical Sight Factory?

Define Your Optical Sight Requirements and OEM Project Goals

Choosing a China top OEM optical sight factory begins with a precise project definition. Clarify the intended use, such as outdoor observation, sports training, surveying, or equipment inspection. Each application demands different optical performance, housing strength, and adjustment control.

Write down measurable requirements before contacting a factory. Include magnification range, objective diameter, field of view, eye relief, reticle style, focusing method, and acceptable weight. Specify materials, surface finish, sealing level, and operating temperatures. Request sample data for brightness, image clarity, parallax behavior, and low-light performance. These details help engineers recommend practical components instead of simply matching a price.

Your OEM goals should also be documented. Decide whether you need a new design, modified components, custom packaging, or complete production support. Ask about prototype timing, inspection procedures, calibration records, and batch consistency. A reliable factory should explain tolerances clearly and provide test evidence. It should also support applicable product safety, import, labeling, and environmental requirements for your target market.

Our early project plans were sometimes too ambitious. We requested premium performance without allowing enough space, power, or budget. That created avoidable revisions. A better approach is to rank requirements as essential, preferred, and optional. Share drawings, reference samples, and usage conditions honestly. Include expected annual volume and delivery needs. A factory can only quote accurately when the project goals are realistic and complete.

Assess Factory Experience, Production Capacity, and Technical Expertise

Choosing a China top OEM optical sight factory requires more than comparing quotations. Examine its experience with your product category, materials, and target market. Ask for dated project records, sample development notes, and quality data. A factory that explains past failures earns more trust than one showing polished photographs. Request references where possible, then verify them independently. Real experience leaves evidence.

Production capacity should be measured on the factory floor, not in a sales presentation. Check machining equipment, coating lines, assembly stations, and inspection areas. Ask about monthly output at your required specification, not maximum theoretical output. Review staffing during peak seasons and backup plans for component shortages. A clean line helps, but it does not prove consistency. Inspect several production batches and compare measurements.

Technical expertise appears in tolerances, testing methods, and engineering communication. Confirm whether the factory can manage optical alignment, shock and vibration testing, sealing checks, and repeatable calibration for lawful civilian applications. Ask for inspection reports, calibration records, and a clear corrective-action process. Engineers should explain why a design may fail, not simply promise success. I would also order a small pilot run before committing to volume. It costs more initially. However, it may expose weak process control early. Factory audits can miss inconvenient details, so keep questioning.

Verify Quality Control Systems, Certifications, and Product Testing

How to Choose a China Top OEM Optical Sight Factory?

A reliable OEM optical sight factory should show its quality system, not just display polished samples. Ask for a current ISO 9001 certificate and verify the issuing body independently. The certificate should match the factory’s legal name, address, and production scope. Check calibration records for collimators, spectrometers, torque tools, and environmental chambers. Small gaps matter.

Product testing must reflect real field conditions. Request inspection data for lens clarity, light transmission, reticle accuracy, adjustment repeatability, and waterproof performance. A serious factory can explain test methods, acceptance limits, and sampling rates in plain language. It should also provide traceability from glass batches to finished units. Look for serialized inspection reports, not generic spreadsheets.

Visit the production line if possible. Observe dust control, alignment benches, sealing procedures, and final visual inspection. Ask how rejected units are isolated and how corrective actions are documented. Some factories report only successful tests. That is not enough. Failed samples can reveal more than perfect charts. A useful audit may uncover inconsistent torque, rushed adhesive curing, or unclear operator instructions. These weaknesses do not always mean the factory is unreliable, but they require evidence of improvement. Independent pre-shipment testing adds another layer of confidence, especially when specifications are customized.

How to Choose a China Top OEM Optical Sight Factory? - Verify Quality Control Systems, Certifications, and Product Testing

Evaluation Dimension What to Verify Credible Evidence Practical Acceptance Criteria Recommended Verification Method Risk if Not Verified
Quality Management System Whether documented procedures control design, purchasing, production, inspection, nonconformities, and corrective actions. Valid ISO 9001 certificate, certification scope, issuing body, audit status, quality manual, and controlled work instructions. Certificate is current, scope covers optical or precision manufacturing, and procedures are implemented on the production floor. Check the certificate with the issuing certification body and perform a video or in-person process audit. Inconsistent batches, undocumented changes, and weak corrective-action control.
Measurement and Calibration How the factory measures optical alignment, dimensions, torque, illumination, and environmental performance. Calibration records, equipment list, traceability certificates, and laboratory accreditation where applicable. Critical instruments have defined calibration intervals and traceability to national or international measurement standards. Review sample calibration certificates and confirm that instruments are within their calibration dates. False pass results, aiming-point variation, and undetected dimensional defects.
Optical Performance Clarity, magnification accuracy, field of view, eye relief, reticle definition, light transmission, and parallax behavior. Inspection records, optical test procedures, measured data, approved samples, and lot-specific test reports. Measured values must meet the agreed product specification and remain consistent across production lots. Compare factory measurements with independent sample testing before mass production. Poor image quality, inconsistent reticle position, or performance below the stated specification.
Mechanical Reliability Turret repeatability, adjustment tracking, mounting interface strength, focus-ring durability, and resistance to vibration. Design validation reports, endurance-test records, torque specifications, and engineering change records. Results meet the agreed test plan with documented sample size, test conditions, measurements, and failure criteria. Witness a repeatability test and inspect retained samples after endurance testing. Point-of-aim shift, loose controls, damaged threads, or failure during use.
Environmental Testing Resistance to temperature cycling, humidity, rain, dust, corrosion, and transport vibration. Environmental chamber records, ingress-protection test reports where claimed, corrosion results, and inspection photos. Test conditions, duration, sample identification, pre-test and post-test measurements, and acceptance limits are documented. Use an independent laboratory for critical claims or request witnessed testing against an agreed standard. Fogging, water ingress, coating failure, corrosion, or loss of optical alignment.
Laboratory Competence Whether internal or external laboratories can produce technically valid and traceable test results. ISO/IEC 17025 accreditation, accredited scope, test methods, equipment records, and laboratory quality controls. The accreditation scope must cover the specific test method and measured characteristic; accreditation is not assumed from a laboratory name alone. Verify the accreditation directory entry and compare the report details with the accredited scope. Test reports may be unsuitable for regulatory, contractual, or technical decisions.
Incoming Material Control Control of optical glass, aluminum or steel parts, coatings, electronics, seals, batteries, and packaging materials. Approved supplier list, incoming inspection records, material certificates, sampling plans, and quarantine procedures. Critical materials are inspected before release and are traceable to supplier lots and purchase orders. Sample recent receiving records and trace one component from receipt to finished product. Hidden material substitutions, coating defects, and variable product performance.
Process Control and Traceability Whether work instructions, operator qualifications, batch identification, and inspection gates are controlled. Production travelers, serial or lot numbers, first-article records, in-process inspection sheets, and operator training records. Finished units can be traced to key materials, operators, equipment, inspection results, and rework history. Conduct a traceability exercise using a randomly selected finished unit. Root-cause investigations become difficult and defective lots may not be contained quickly.
Final Inspection and Acceptance Inspection of appearance, dimensions, optical function, reticle operation, packaging, labels, and accessories. Signed final inspection reports, sampling plan, defect classification, photographs, and shipment release records. Acceptance limits are defined before production and critical defects are not accepted without written approval. Approve a pre-shipment inspection checklist and use an independent inspection agency when appropriate. Cosmetic defects, missing parts, incorrect configurations, and avoidable customer complaints.
Certification and Regulatory Fit Whether required certifications and declarations apply to the exact product, market, configuration, and electrical features. Current certificates, declarations of conformity, technical files, test reports, and certification scope. Documents identify the correct model, revision, rated input, applicable directives or standards, and responsible legal entity. Confirm requirements for the destination market with an accredited testing or compliance specialist. Customs delays, product recalls, market-access problems, or misleading compliance claims.
Corrective and Preventive Action How the factory handles complaints, recurring defects, root-cause analysis, containment, and effectiveness checks. Nonconformance reports, 8D or equivalent reports, corrective-action logs, and trend analysis. Actions identify the root cause, responsible owner, deadline, containment step, and objective evidence of effectiveness. Review anonymized examples of closed corrective actions and verify whether similar defects recurred. Repeated quality failures and slow resolution of field problems.
OEM Engineering and Change Control Ability to manage drawings, tolerances, firmware or reticle revisions, tooling changes, and customer approvals. Controlled drawings, revision history, engineering change notices, prototype reports, and approval records. No critical change is implemented without documented review, risk assessment, validation, and customer authorization where required. Request a redacted example of an engineering change process and compare the approved sample with production units. Unapproved substitutions, compatibility problems, and differences between samples and mass production.
Supplier and Production Capacity Availability of critical equipment, skilled personnel, backup processes, and capacity for stable delivery. Capacity plan, equipment maintenance records, staffing plan, production schedule, and supplier continuity assessment. Capacity claims are supported by equipment, labor, cycle-time, and inspection-resource data rather than estimates alone. Compare forecast demand with demonstrated output and identify single-source components. Late delivery, rushed inspections, unauthorized outsourcing, and quality deterioration during peak demand.
Pre-Production Validation Whether samples represent the final materials, tooling, processes, software, packaging, and inspection requirements. Approved golden sample, first-article inspection report, pilot-run data, reliability results, and signed specification. Mass production begins only after the pilot lot meets agreed functional, dimensional, cosmetic, and packaging requirements. Test pilot units independently and retain sealed reference samples for future comparison. Production units may differ from approved samples in function, finish, or configuration.
After-Sales and Warranty Support Availability of repair procedures, spare parts, failure analysis, warranty terms, and response-time commitments. Written warranty policy, service workflow, spare-parts list, failure-rate reports, and customer complaint records. Responsibilities, response times, repair or replacement conditions, and return procedures are defined in the supply agreement. Review anonymized service cases and include measurable support obligations in the contract. High service costs, unresolved field failures, and customer dissatisfaction.
Selection principle: Treat certificates as evidence of a management or laboratory system, not as proof that every optical sight meets your requirements. Confirm the exact product specification through independent testing, production audits, traceability reviews, and pre-shipment inspection.

Review Customization Services, Prototypes, and Manufacturing Support

Choosing a China top OEM optical sight factory requires more than comparing prices. Review its customization process, prototype discipline, and manufacturing support before signing any agreement. A capable factory should discuss lens requirements, housing materials, reticle preferences, sealing, and mounting dimensions clearly. It should also confirm which specifications are technically realistic.

Prototype quality reveals engineering maturity. Ask for a sample with documented measurements, coating details, focus performance, and environmental test results. Inspect the adjustment feel, image clarity, edge distortion, and finish under different lighting. Small defects often appear around threads, seals, or adjustment controls. These details matter during long-term field use. No factory is perfect, but reliable teams record problems and correct them quickly.

Tips: Request a written prototype schedule and revision history. Confirm inspection standards, production tolerances, packaging, spare-part support, and after-sales response times. Ask whether engineers can provide drawings, test reports, and controlled sample approvals. Manufacturing support should continue after the first order, including process updates and quality feedback. A factory that avoids difficult questions may create expensive delays later. I would also leave room for revision; early assumptions are sometimes wrong, especially when a prototype behaves differently from its drawing. Ensure all products, testing, and final use comply with applicable laws and safety requirements.

Compare Pricing, Communication, Lead Times, and Contract Terms

Choosing a China-based OEM optical sight factory requires more than a low quotation. In my sourcing work, I compare the full landed cost, not only the unit price. Ask whether tooling, optical coating, inspection, packaging, and sample fees are included. A cheap quote can become expensive after revisions. Request a line-by-line offer with currency, payment stages, minimum order quantity, and warranty coverage. Keep records. Written communication matters. A capable sales engineer should explain mounting dimensions, reticle options, tolerances, and testing methods in clear English. If answers change between email and video calls, slow down.

Lead time deserves the same scrutiny. Ask for separate dates for drawing approval, sample production, pilot production, and mass delivery. Request evidence from recent, comparable orders while protecting confidential information. A factory should identify inspection points, such as lens alignment, adjustment tracking, sealing, and drop testing. Verify these details through a sample report or live factory call. I once treated an attractive sample as proof of stable production. That was too optimistic. Production consistency needs its own evidence. Build buffer time for holidays, component shortages, and rework. Do not promise customers a date based on the best-case schedule.

Contract terms protect both sides when specifications are precise. Define approved drawings, materials, tolerances, acceptance criteria, change-control procedures, late-delivery remedies, and defect replacement. State who owns tooling and technical files. Clarify inspection rights before shipment and payment conditions after acceptance. Include confidentiality and compliance obligations for each destination market. Confirm export documents and applicable laws with qualified professionals. Small wording differences matter. Some factories resist detailed clauses, and that resistance is useful information. Still, rigid terms can damage cooperation when they ignore practical production limits. A balanced contract allows documented corrections without weakening quality requirements.

Amet mattis vulputate enim nulla aliquet. Id porta nibh venenatis cras sed felis dictumst vestibulum rhoncus est.
This error message is only visible to WordPress admins

Error: No feed found.

Please go to the Instagram Feed settings page to create a feed.

Quick links