OPEN FROM 9AM TO 5PM – CLOSED ON WEEKENDS
Choosing the right MCB Riveting Machine in 2026 requires more than comparing prices or advertised cycle times. Manufacturers must connect machine capability with product quality, operator safety, maintenance access, and long-term production goals. A reliable decision begins with the MCB design, including rivet diameter, contact arrangement, housing material, and required assembly tolerances. Small differences matter. A loose rivet may affect contact stability, while excessive force can deform sensitive components.
Experienced buyers should examine the complete riveting process, not only the press itself. Ask suppliers to demonstrate automatic feeding, rivet orientation, stroke control, force monitoring, and finished-part inspection. A clear data trail is valuable. Production records should identify batch numbers, tooling changes, measured force, and rejected units. These details support quality investigations and strengthen process accountability. They also reveal whether the machine performs consistently after several hours, not just during a short demonstration.
Look closely at changeover time. Different MCB models may require adjustable tooling, guided fixtures, or quick replacement components. Practical features, such as guarded access, emergency stopping, sensor diagnostics, and simple lubrication points, can reduce daily risks and downtime. However, no machine is perfect. Marketing claims may omit noise, feeding interruptions, or difficult cleaning tasks. Request representative samples and realistic factory trials before purchasing. Review supplier experience, technical documentation, spare-parts support, training, and validation methods. The best MCB Riveting Machine is not always the fastest option. It is the one that delivers stable joints, measurable results, safe operation, and dependable support throughout its working life.
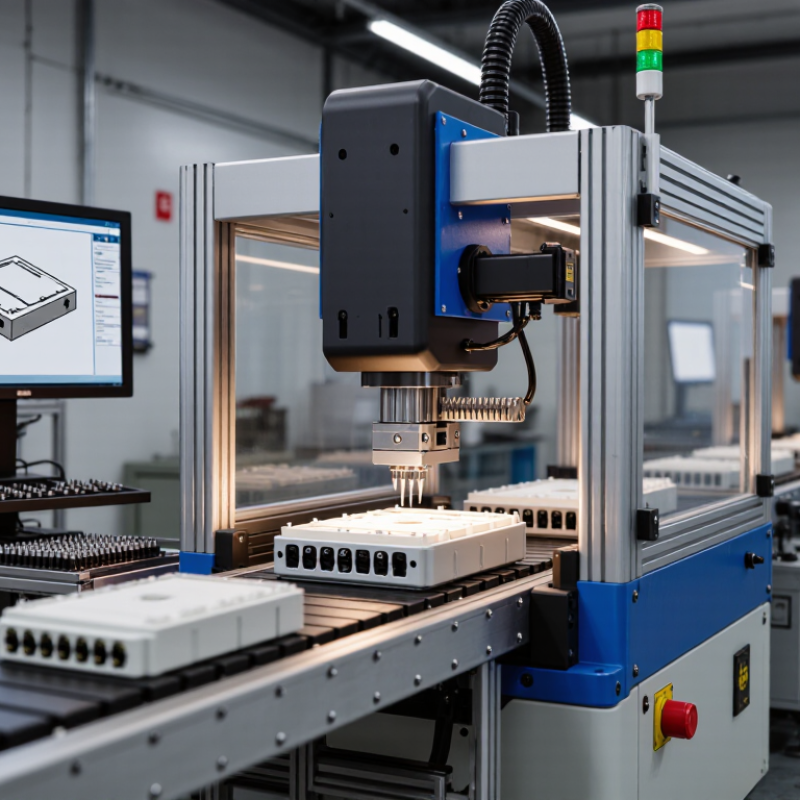
MCB riveting machines generally fall into pneumatic, hydraulic, electric servo, and rotary indexing types. Pneumatic models suit stable, medium-volume production with simple rivet loads. Hydraulic machines deliver stronger forming force for thicker metal parts. Servo-electric systems provide accurate stroke control, lower noise, and useful production data. Rotary indexing machines handle several assembly steps in one cycle. They work well for high-volume MCB production.
Application conditions should guide the choice. A single-spindle machine fits small batches, laboratory trials, and frequent product changes. Multi-spindle equipment can rivet several points together, reducing cycle time and alignment errors. For one-pole and two-pole MCBs, confirm the machine’s fixture range, rivet diameter, and feeding method. Automatic bowl feeders help continuous lines, while manual loading may be more practical for varied orders. Keep the operator’s access clear.
Check force consistency, stroke repeatability, guarding, and maintenance access before purchase. A force sensor can identify loose or crushed rivets during production. Traceable settings also support quality audits and process improvement. In my experience, many failures begin with poor fixture design, not the riveting head. A fast machine is not always the best machine. Some suppliers promise impressive output, yet they test with ideal parts and clean feeding systems. Request samples using your actual MCB housings, terminals, and rivets. Then inspect pull strength, deformation, noise, and cycle stability over several hours.
How to Choose a MCB Riveting Machine in 2026?
Selecting an MCB riveting machine starts with the breaker design, not the machine’s advertised speed. Confirm pole count, housing dimensions, rivet material, rivet diameter, and contact-stack height. IEC 60898-1 requirements also make consistent mechanical assembly essential for miniature circuit breakers. A machine must control riveting force, stroke, alignment, and indexing within repeatable limits.
In my commissioning experience, a compact MCB often needs more careful tooling than a larger product. A small offset of 0.1 mm can deform the rivet head or restrict contact movement. Small errors matter. Select adjustable fixtures for different case geometries. Check whether the machine supports copper, brass, or plated rivets without changing the entire feeding system. According to World Robotics 2024, 541,302 industrial robots were installed globally in 2023. That figure supports automation, but automation alone does not guarantee quality.
Tips: Request sample trials using your actual MCB shells and rivets. Measure pull-out strength, head diameter, contact travel, and electrical continuity after riveting. Ask for force-displacement records and batch traceability. Review changeover time, spare tooling, and operator access. Fit beats speed. A high-output machine may still be unsuitable if its feeder damages soft rivets. I would also test imperfect parts deliberately. Real production includes burrs, slight molding variation, and inconsistent plating. Ignore those conditions, and the machine may pass laboratory trials but struggle on the factory floor.
Match Machine Specifications to MCB Design Requirements
The chart compares representative engineering requirements for 1-pole to 4-pole MCB assemblies. As pole count increases, the machine generally needs higher riveting force, greater working width, and more riveting positions. Select a machine with sufficient force reserve, adjustable stroke, accurate positioning, and a cycle time that supports the required production rate.
Reference values are representative planning targets for machine selection. Final specifications should be verified against the actual MCB drawing, rivet material, contact geometry, and validated process tests.
Riveting quality should be measured, not assumed. A reliable machine controls riveting force, stroke, and head height on every cycle. Check sample joints under magnification. The rivet should sit evenly, without cracks, loose terminals, or distorted plastic. IEC 60898-1 provides a useful reference for low-voltage circuit-breaker performance, but the machine still needs process validation. Ask for recorded force-displacement curves, dimensional data, and rejection samples. No machine is perfect.
Accuracy matters when small deviations affect contact pressure and electrical safety. Look for servo-driven positioning, automatic fixture alignment, and sensors that detect missing parts. A practical acceptance test can inspect 1,000 consecutive assemblies, then compare height, diameter, and pull-out strength. Define limits before testing. This prevents attractive but vague claims. Statistical process control is helpful, though operators may not maintain it consistently.
Capacity must match real demand, not brochure speed. Calculate usable cycles after loading, inspection, stoppages, and changeovers.
The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, a 10% annual increase in automation adoption. Deloitte’s 2024 Smart Manufacturing and Operations Survey found 86% of manufacturing executives view smart manufacturing as important for competitiveness.
Choose a riveting system with traceability, alarm history, and quick tooling changes. A machine rated at 30 cycles per minute may deliver far less in production. Test it with your actual MCB components, operators, and shift conditions.
How to Choose a MCB Riveting Machine in 2026?
Compare Automation, Safety Features, and Maintenance Needs
Choosing an MCB riveting machine in 2026 requires more than checking output speed. Compare semi-automatic and fully automatic systems against your actual production volume, product range, and operator skills. A fully automated line may reduce handling, but it can increase setup complexity. Semi-automatic equipment often gives technicians better control during frequent product changes. That flexibility matters.
Safety deserves careful inspection. Look for guarded riveting areas, reliable interlocks, emergency stops, and clear fault indicators. The machine should stop when a door opens, not continue through a cycle. Check whether sensors detect missing components before riveting. Small gaps in detection can create expensive defects. Ask for risk assessment records, operator training guidance, and practical access for cleaning. A polished demonstration proves little.
Maintenance needs equal attention. Examine how easily workers can reach tooling, pneumatic lines, electrical cabinets, and lubrication points. Tool replacement should not require dismantling half the machine. Built-in diagnostics can shorten troubleshooting, especially when error codes identify pressure loss or sensor failure. Keep critical wear parts available, with documented service intervals. In my experience, neglected cleaning causes more downtime than dramatic mechanical failures. Still, this is easy to underestimate. A compact design may look efficient, yet cramped access can slow every repair. Request a sample cycle using your own MCB components. Measure noise, cycle stability, changeover time, and defect handling before making a decision.
| Machine Configuration | Typical Automation Level | Typical Output Range* | Operator Involvement | Riveting Process Control | Key Safety Features to Verify | Changeover and Setup | Maintenance Needs | Best-Fit Production Scenario | Selection Assessment |
|---|---|---|---|---|---|---|---|---|---|
| Manual Bench Riveting Machine | Manual loading and unloading; pneumatic or electric riveting cycle | Approximately 300–800 MCB units per hour, depending on product design and operator speed | High; the operator positions each component and starts or confirms the cycle | Basic force, stroke, or time adjustment; limited automatic data collection | Two-hand start or guarded trigger, emergency stop, point-of-operation guarding, and adjustable pressure regulator | Fast and economical for one or a few product variants | Daily cleaning and visual checks; periodic inspection of tooling, air lines, fasteners, and lubrication points | Low-volume production, prototyping, repair work, and frequent product changes | Suitable when initial investment and flexibility are more important than maximum throughput |
| Semi-Automatic Indexing Machine | Automatic riveting cycle with manual component loading and unloading | Approximately 800–1,800 MCB units per hour, subject to the number of rivets and loading time | Medium; the operator loads parts while the machine controls the programmed cycle | Programmable stroke, dwell time, pressure, indexing position, and cycle confirmation | Interlocked guard, safety relay, emergency stop, part-presence sensor, anti-repeat control, and overload protection | Moderate; dedicated fixtures improve repeatability but may require tooling changes between variants | Routine cleaning, air-filter and regulator checks, fixture inspection, sensor testing, and scheduled tooling replacement | Small- to medium-batch manufacturing with several MCB configurations | A balanced choice for improving consistency without the complexity of a fully automatic line |
| Automatic Rotary-Indexing Riveting Line | Automatic feeding, indexing, riveting, inspection, and part discharge | Approximately 1,500–3,500 MCB units per hour, depending on station count and product geometry | Low during normal operation; staff mainly replenish components, monitor alarms, and perform quality checks | PLC-controlled sequence with programmable force or pressure, stroke position, cycle time, and fault logging | Full perimeter guarding, interlocked access doors, safety-rated control circuit, light curtains where required, jam detection, and emergency stops | Slower and more involved; product-specific nests, feeders, and programs may need adjustment | Scheduled preventive maintenance for feeders, indexing drives, pneumatic circuits, sensors, tooling, and safety devices | Medium- to high-volume production with stable product designs and predictable demand | Strong option when labor reduction, repeatability, and continuous production justify higher capital cost |
| Servo-Controlled Automated Cell | High automation with servo riveting, robotic or automatic loading, inspection, and traceability functions | Approximately 1,000–3,000 MCB units per hour, depending on inspection, feeding, and handling requirements | Low; operators supervise the cell, replenish materials, and respond to diagnostic messages | Closed-loop control can monitor force, position, speed, and cycle signature for each riveting operation | Risk-assessed guarding, safety PLC, interlocked doors, light curtains or scanners, safe torque off, two-channel emergency stops, and controlled restart | Moderate to complex; recipe-based setup can shorten changes, but fixtures and automation programs require validation | Planned servicing of servo drives, sensors, robots or actuators, software backups, tooling, feeders, and safety circuits | High-quality production where process traceability, low defect rates, and digital manufacturing data are priorities | Best for demanding production environments with sufficient technical support and maintenance capability |
| Modular Multi-Station System | Configurable automation combining riveting with feeding, screwdriving, testing, marking, or visual inspection | Approximately 700–2,500 MCB units per hour, depending on the slowest station and inspection requirements | Low to medium; loading may be manual or automatic, while integrated stations run in sequence | Station-level parameters, interlocks, reject handling, and optional barcode or recipe management | Guarded modules, station interlocks, safety-rated stop functions, jam detection, reject confirmation, and safe access for maintenance | Flexible when modules and fixtures are designed for future product variants | Each module requires its own inspection schedule; spare-part planning is important because several technologies may be integrated | Manufacturers seeking one expandable platform for assembly, riveting, testing, and quality control | Recommended when future expansion and process integration are more valuable than the simplest machine architecture |
*Output figures are typical planning ranges rather than guaranteed capacities. Actual performance depends on the number and type of rivets, component tolerances, feeding method, fixture design, operator loading time, inspection requirements, and applicable machine-safety regulations. Before purchase, request a documented cycle-time study, sample-part trial, risk assessment, spare-parts list, and preventive-maintenance schedule.
The purchase price is only one part of a riveting machine’s real cost. Compare output, energy use, tooling life, maintenance, and operator training. A machine costing 20% less may require frequent adjustments and expensive downtime. Ask suppliers for measured cycle times, not optimistic estimates. Request sample riveted assemblies from your own MCB components. Check rivet height, alignment, and surface damage under normal production conditions.
Supplier quality matters as much as machine design. Evaluate technical drawings, factory testing records, spare-part availability, and response times. A reliable supplier should explain fixture replacement, software updates, and safety checks clearly. Avoid vague promises. They create risk. Speak with current users, if possible, and ask about support after installation. Their experience may reveal delays that sales documents never mention.
Long-term operating value depends on stable performance. Choose equipment with accessible wear parts, simple diagnostics, and adjustable riveting pressure. Sensors should detect missing components before defective units reach inspection. Calculate labor savings over several years, but include calibration and unplanned stoppages. A spreadsheet can look convincing. Reality is less tidy. Production volumes may change, and a highly automated machine could become underused. Leave room for future tooling, but do not pay for features your line will never use. Perform a total-cost review every year.

