OPEN FROM 9AM TO 5PM – CLOSED ON WEEKENDS

What Are the 2026 Top GRP Gutter Machinery Types?

What Are the 2026 Top GRP Gutter Machinery Types? This question matters to manufacturers seeking cleaner production, stable quality, and better control over operating costs. GRP, or glass-reinforced plastic, requires equipment that handles resin, glass reinforcement, curing, trimming, and finishing with precision. Grp Gutters Machinery now includes pultrusion lines, continuous profile systems, resin mixing units, cutting machines, and automated inspection equipment. Each type supports a different production stage.

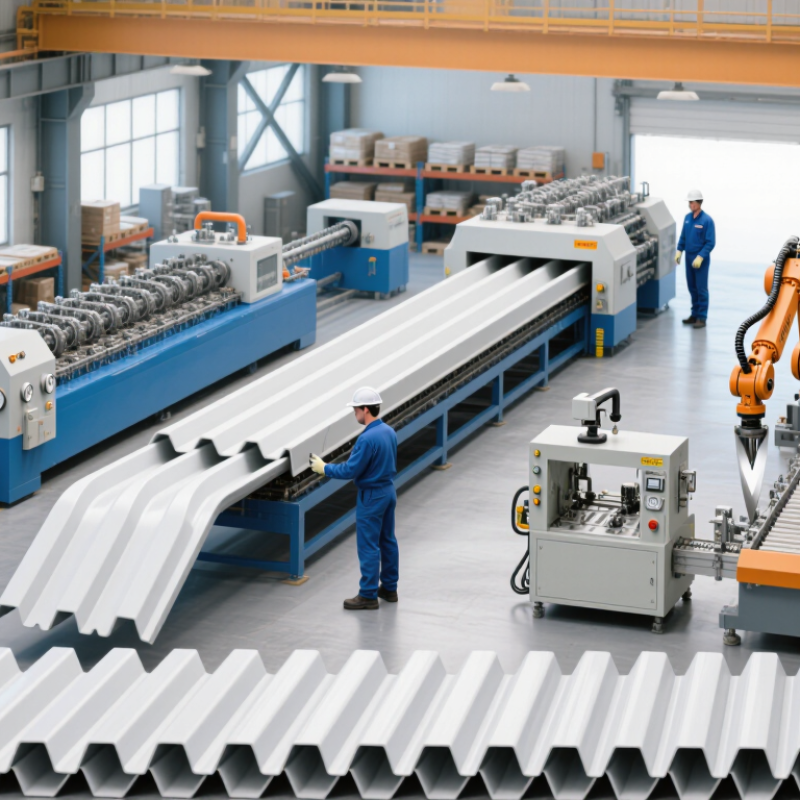
In practical workshops, a pultrusion line may draw glass fibers through a resin bath before shaping them through heated dies. The finished gutter emerges continuously, with its profile formed under controlled pressure and temperature. Continuous forming equipment suits larger orders, while cutting and drilling machines help prepare consistent outlet openings and connection points. Automation can reduce manual variation, but it does not remove the need for skilled supervision. Small errors matter.

A reliable 2026 machinery review should examine output speed, energy use, mold flexibility, maintenance access, and worker safety. It should also consider resin waste and the availability of replacement components. Some suppliers promote impressive capacity figures, yet real performance may change with gutter dimensions, resin formulation, and operator experience. That deserves careful reflection. Buyers should compare verified production data, test samples, warranty terms, and technical support before choosing equipment. The “top” machine is not always the fastest. It is the system that delivers repeatable profiles, clean edges, and dependable long-term operation.
What Are the 2026 Top GRP Gutter Machinery Types?

GRP Gutter Machinery in 2026: Classify Lines by Forming Method

GRP Gutter Machinery in 2026: Classify Lines by Forming Method

GRP gutter machinery is best classified by how it shapes the profile, not by output speed alone. Pultrusion lines pull resin-impregnated glass fibers through a heated die. They produce continuous gutters with steady wall thickness and strong longitudinal reinforcement. A typical line includes creels, resin baths, preform guides, a heated die, pullers, and a cutting station. According to the Research and Markets Pultrusion Global Market Report 2024, the pultrusion market was valued at about USD 3.4 billion in 2023. That growth reflects demand for durable composite profiles.

Continuous molding lines use controlled resin application, surface films, heating, and calibrated rollers. They suit wider gutter profiles and textured outer surfaces. Compared with pultrusion, their fiber alignment can be less uniform. That weakness matters near brackets and outlet openings. Compression molding systems shape short GRP sections inside matched heated molds. They work well for end caps, corners, outlets, and other detailed fittings, rather than long gutters. The Composites Market Report by Grand View Research identified construction as a major composites application sector, with infrastructure renewal supporting continued demand.

Line selection should follow the product drawing. Check resin viscosity, glass content, die temperature, puller pressure, and cut-length tolerance. A production trial should inspect a 600-millimeter sample after cooling. Small distortions may appear later. I would not choose machinery from catalog speed alone. Energy use, mold-change time, scrap handling, and operator access often decide the real cost.

Pultrusion Machines: Compare 0.5–2.0 m/min Profile Production Rates

What Are the 2026 Top GRP Gutter Machinery Types?

Pultrusion Machines: Compare 0.5–2.0 m/min Profile Production Rates

Pultrusion machines remain central to GRP gutter production in 2026. Their practical output usually ranges from 0.5 to 2.0 m/min, depending on profile depth, resin chemistry, and glass content. A compact single-line machine often suits standard gutter sections at 0.5–1.0 m/min. It offers easier setup and more controlled material changes.

Faster systems can reach 1.2–2.0 m/min with stable heating and servo-controlled pulling. Dual-line equipment may produce two smaller profiles together, improving floor-space efficiency. However, higher speed is not automatically better. The die may overheat, the surface can lose gloss, and dimensional drift may appear near corners. Slow down when the profile becomes uneven.

Experienced operators check the puller pressure, die temperature, and fiber alignment during every shift. A simple gauge can reveal width changes before packaging begins. I have found that 0.8–1.2 m/min often provides a useful balance between output and finish quality. This is not a fixed rule. Thick wall sections, recycled fillers, or complex reinforcement layouts can change the result.

Machine selection should also consider cutting accuracy, cooling length, and maintenance access. A reliable line needs steady tension, clean guides, and repeatable curing conditions. Production records should connect speed with scrap rate, surface defects, and final profile measurements. That evidence is more valuable than a headline capacity figure.

Resin Mixing Systems: Evaluate 2–5% Catalyst-Dosing Accuracy

What Are the 2026 Top GRP Gutter Machinery Types?

Resin Mixing Systems: Evaluate 2–5% Catalyst-Dosing Accuracy

In 2026, GRP gutter machinery will be judged by consistency, not speed alone. Resin mixing systems deserve close attention. At a 2–5% catalyst setting, a small dosing error can change gel time and surface quality. Too little catalyst may leave soft, under-cured sections. Too much can shorten working time and increase heat. Both outcomes waste material.

Grand View Research’s 2024 market assessment placed the global composites market near US$110 billion in 2023. It also forecast annual growth of about 7% through 2030. This expansion increases pressure on small production lines. Operators should test dosing accuracy at 2%, 3.5%, and 5%, rather than only checking the midpoint. Use gravimetric weighing, temperature logs, and timed collection tests. ASTM D2471 can help verify gel time and exothermic behavior after adjustments. A clean dashboard does not prove good mixing. We still need physical samples.

Tips: Keep catalyst hoses short and shaded. Check actual mass, not pump display values. Recalibrate after maintenance. Record resin temperature beside every test result. Do not trust old settings. A minor correction may improve stability, but excessive automation can hide poor operator judgment.

What Are the 2026 Top GRP Gutter Machinery Types? — Resin Mixing Systems: Evaluate 2–5% Catalyst-Dosing Accuracy
Machinery Type Typical GRP Gutter Process Resin Mixing System Catalyst-Dosing Accuracy Typical Output Range Best-Fit Production Requirement Evaluation Notes
Continuous Pultrusion Line Continuous profile forming with resin impregnation, heated shaping, curing, pulling and cutting. Metered resin-and-catalyst dosing unit with static or dynamic mixing head. Typically ±1–2% of setpoint Approx. 50–250 kg/h Long, constant-profile gutters requiring high dimensional consistency and continuous production. A strong choice when the resin-to-catalyst ratio must remain stable during long production runs. Closed-loop flow measurement is preferred.
Continuous Wet-Out and Forming Line Fiberglass reinforcement is wetted, shaped around a profile, consolidated and cured in a continuous line. Gravimetric or Coriolis-based resin delivery with separate catalyst metering. Typically ±0.5–1.5% of setpoint Approx. 30–180 kg/h Medium- to high-volume production with tight control of glass content and resin consumption. Useful where laminate uniformity is critical. The system should compensate for changes in resin viscosity, temperature and line speed.
Pultrusion Resin-Injection System Resin is injected into a closed impregnation die or injection chamber around continuous glass reinforcement. Pressurized two-component metering and mixing system with injection-pressure monitoring. Typically ±1–2% of setpoint Approx. 40–200 kg/h Low-void structural gutters and profiles with controlled fiber wet-out. The mixing system should maintain a consistent catalyst ratio without excessive residence time, which can cause premature gelation.
Compression Molding Cell Preformed charge, sheet molding compound or wet laminate is pressed in a heated mold to create gutter sections or fittings. Batch resin preparation or automated premix system with weight-based catalyst addition. Typically ±1–3% of setpoint Approx. 5–60 kg per charge Short runs, complex fittings, end caps, outlets and products needing repeatable mold filling. Batch weighing is generally adequate for 2–5% catalyst targets when the scale resolution and mixing sequence are properly controlled.
Resin Transfer Molding Cell Dry reinforcement is placed in a closed mold and resin is injected under controlled pressure or vacuum assistance. Two-component metering unit with static mixer, pressure control and resin-temperature conditioning. Typically ±1–2% of setpoint Approx. 2–40 kg per mold cycle Low- to medium-volume gutter fittings, custom profiles and parts with controlled surface finish. Catalyst accuracy must be considered together with injection time, mold temperature and resin gel time to avoid dry spots or incomplete filling.
Vacuum-Assisted Resin Infusion System Vacuum draws catalyzed resin through dry fiberglass reinforcement inside a sealed mold or bag. Batch catalyst dosing followed by low-shear mixing and controlled resin-feed equipment. Typically ±2–5% of setpoint Approx. 1–25 kg per cycle Large, low-volume gutter sections and tooling where low capital cost and low void content are priorities. The 2–5% accuracy band may be acceptable for many infusion formulations, but catalyst quantity should be verified by weight before the resin enters the laminate.
Automated Batch Resin Mixing Station Resin, catalyst and additives are weighed, mixed and supplied to manual or semi-automatic forming equipment. Load-cell-controlled batch mixer with programmable dosing sequence and agitator. Typically ±1–3% of setpoint Approx. 10–500 kg per batch Flexible production of multiple gutter sizes, colors, resin formulations and repair components. Batch systems offer good formulation flexibility. Agitation time, vessel dead volume and catalyst distribution should be validated during commissioning.
Automated Two-Component Meter-Mix Unit Separate resin and catalyst streams are metered, mixed immediately and delivered to a mold, impregnation zone or applicator. Servo-driven pumps, flow meters and disposable or cleanable static mixer. Typically ±0.5–1.5% of setpoint Approx. 0.5–120 kg/h High repeatability, reduced operator contact and controlled processing of short-pot-life resin systems. This is generally the most precise option for catalyst ratios in the 2–5% range, provided pump calibration and ratio verification are performed regularly.
Robotic Dispensing and Forming Cell Automated resin application, reinforcement placement or bead dispensing is coordinated with mold movement or profile forming. Integrated meter-mix dispenser with recipe control, pressure feedback and automatic purge. Typically ±1–2% of setpoint Approx. 0.2–30 kg/h Custom gutter geometries, frequent product changes and digitally traceable production. Recipe control can reduce operator variation. The system should record actual resin and catalyst consumption rather than relying only on commanded pump speed.
Accuracy values are typical engineering ranges expressed relative to the programmed catalyst setpoint. Actual performance depends on catalyst viscosity, temperature, pump calibration, scale resolution, mixing method, line speed and resin formulation. Final equipment selection should be confirmed through a material-specific trial.

Cutting and Drilling Units: Control ±1 mm Length and Joint Precision

What Are the 2026 Top GRP Gutter Machinery Types?

Cutting and drilling units will define GRP gutter production in 2026. Their value is not speed alone. It is repeatable geometry. A calibrated saw should hold gutter length within ±1 mm, while guided drilling keeps joint holes aligned across repeated sections. In practice, operators need rigid fixtures, carbide tools, dust extraction, and automatic length compensation. Small errors accumulate quickly at corners. They become visible during installation.

A 2024 Fortune Business Insights report estimated the global fiberglass market at about USD 16.6 billion in 2023, with continued growth expected through 2032. This expansion increases pressure for measurable quality control. The most reliable machinery records cutting length, hole position, tool wear, and operator adjustments. Laser measurement or contact probes can verify each batch before packing. Simple checks still matter.

Some workshops overstate ±1 mm performance. The figure may apply only under stable temperature, clean fixtures, and new tooling. GRP dust changes that reality. Reflection is necessary. A practical acceptance plan should inspect several pieces per batch, check diagonal joint alignment, and compare results with calibrated gauges. ISO 9001-based procedures can support traceability, but they cannot replace careful machine setup. Precision begins with restraint.

2026 Top GRP Gutter Machinery Types

Cutting and drilling units are evaluated by dimensional control for GRP gutter profiles. Lower values indicate tighter process accuracy.

The chart compares typical dimensional accuracy targets used in automated GRP profile fabrication: cut-length deviation and joint-hole position deviation, both measured in millimetres. A ±1 mm cut-length target supports consistent joints and reduces trimming during installation.

Quality Inspection Equipment: Verify Wall Thickness, Cure, and Surface Finish

What Are the 2026 Top GRP Gutter Machinery Types?

Quality Inspection Equipment: Verify Wall Thickness, Cure, and Surface Finish

GRP gutter production may use pultrusion, continuous molding, trimming, and drilling equipment. Yet machinery output is only reliable when inspection follows every critical stage. The 2024 AVK Composites Market Report estimated global composite production at approximately 12.5 million tonnes in 2023. That scale increases pressure for repeatable quality control.

Wall thickness needs more than a quick visual check. Ultrasonic thickness gauges can scan cured gutters without cutting samples. Operators should measure near corners, joints, outlets, and trimmed edges. These areas often show resin-rich spots or reinforcement movement. Record several readings per section. One reading can mislead.

Cure verification requires practical evidence. Barcol hardness testing gives a fast shop-floor indication of surface cure, while differential scanning calorimetry can examine residual curing in laboratory samples. The 2024 composites market outlook from a leading industry research publisher projected strong growth through 2028, making traceable testing increasingly important. Surface finish also deserves measurement. Gloss meters, profile comparators, and controlled lighting can reveal waviness, pinholes, and uneven gel-coat coverage. Do not trust appearance alone. It sometimes hides defects. A useful inspection plan combines machine data, dimensional checks, and periodic destructive testing. The plan may still need revision after field feedback.

Amet mattis vulputate enim nulla aliquet. Id porta nibh venenatis cras sed felis dictumst vestibulum rhoncus est.
This error message is only visible to WordPress admins

Error: No feed found.

Please go to the Instagram Feed settings page to create a feed.

Quick links